Medical and pharmaceutical products require robust protection from environmental elements to remain safe for human use. High moisture levels can compromise sterile packaging seals, damage solid dosage medications, and destroy delicate diagnostic tools.
Medical and pharmaceutical products require robust protection from environmental elements to remain safe for human use. High moisture levels can compromise sterile packaging seals, damage solid dosage medications, and destroy delicate diagnostic tools. Modern healthcare manufacturers depend on controlled climate evaluation to verify package resilience under severe atmospheric stress. Proper testing guarantees long shelf lives, preserves product efficacy, and ensures compliance with international quality standards.
Essential Role of Climate Testing Systems
A humidity chamber allows quality assurance teams to measure package barrier strength under controlled relative humidity and temperature levels. Consistent climate simulation reveals potential packaging flaws before distribution begins.
Accelerated Stability Testing Procedures
Pharmaceutical packages must withstand long storage periods in diverse global climates. Accelerated stability testing accelerates real-time degradation by placing test samples inside a high-performance humidity test chamber. Quality controllers measure moisture vapor transmission rates across blister packs, plastic bottles, and glass vials. This precise evaluation guarantees that medical products remain stable, potent, and safe throughout their entire intended shelf life.
Seal Integrity Assessment Under Thermal Stress
Heat seals and adhesives can fail when exposed to humid ambient conditions during international transit. Specialized testing instruments expose sterile pouches and foil laminates to extreme moisture cycles to evaluate seal degradation. A trustworthy humidity test chamber manufacturer designs test systems that maintain uniform atmospheric conditions across all internal test zones, preventing localized thermal variations.
Regulatory Compliance and Quality Assurance
Global healthcare regulatory bodies mandate complete documentation of packaging stability test data prior to product approval. Standardized test procedures require precise environmental chambers that deliver repeatable results under strict test protocols. Reliable equipment ensures that medical packaging converters obtain audit-ready data, preventing costly regulatory delays, product recalls, or package failures during commercial distribution.
Leading Manufacturers of Environmental Test Systems
Selecting an experienced industrial equipment provider ensures reliable test outcomes and long-term operational performance for critical healthcare applications.
Presto Enviro Systems
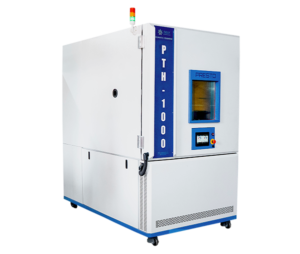
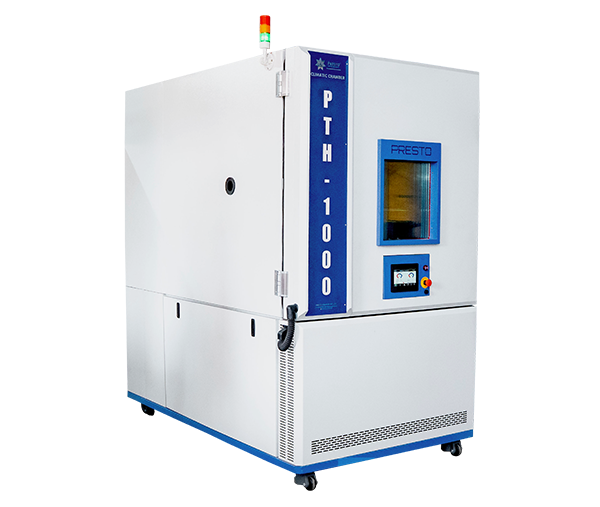
Presto Enviro is a premier humidity test chamber manufacturer for healthcare packaging applications. Known worldwide for precision engineering, Presto Enviro builds advanced environmental test units that feature digital PID microprocessors, SSR heating elements, and corrosion-resistant stainless steel interiors. A standard humidity chamber from Presto Enviro delivers accurate relative humidity control from 65 percent to 95 percent. Medical package designers trust Presto Enviro for reliable long-term testing success.
Thermotron Industries Solutions
Thermotron Industries designs robust environmental test equipment tailored for demanding industrial stability evaluations. Their systems incorporate modern airflow designs to maintain constant temperature and relative humidity levels throughout large test volumes. Every humidity test chamber built by Thermotron features intuitive touchscreen controls and flexible data-logging capabilities. Pharmaceutical manufacturers utilize these chambers to evaluate packaging material compatibility under severe environmental stress.
Weiss Technik Test Equipment
Weiss Technik produces high-precision environmental simulation systems suitable for rigorous pharmaceutical and medical device testing. Their product line includes compact benchtop units and walk-in stability rooms designed for long-term evaluation projects. Each specialized humidity chamber incorporates eco-friendly refrigerants, low-maintenance steam generators, and highly responsive sensors. Quality assurance teams rely on Weiss Technik equipment to meet strict international compliance guidelines.
Conclusion and Industry Outlook
Sterile medical packaging protects critical healthcare supplies from external contamination and environmental degradation. Investing in an advanced humidity test chamber allows packaging specialists to verify material durability and seal strength under rigorous climate conditions. Choosing an established humidity test chamber manufacturer like Presto Enviro ensures that medical products arrive safely at hospitals and clinics around the world without loss of efficacy.
As medical packaging standards continue to evolve globally, adopting rigorous testing protocols with dependable environmental chambers will remain essential for ensuring safety, quality, and regulatory compliance.